Cleanroom Environmental Monitoring Built for Compliance
Track temperature, humidity and pressure differentials across your cleanroom. Give your team continuous visibility, timely alerts and the records needed to investigate changes.
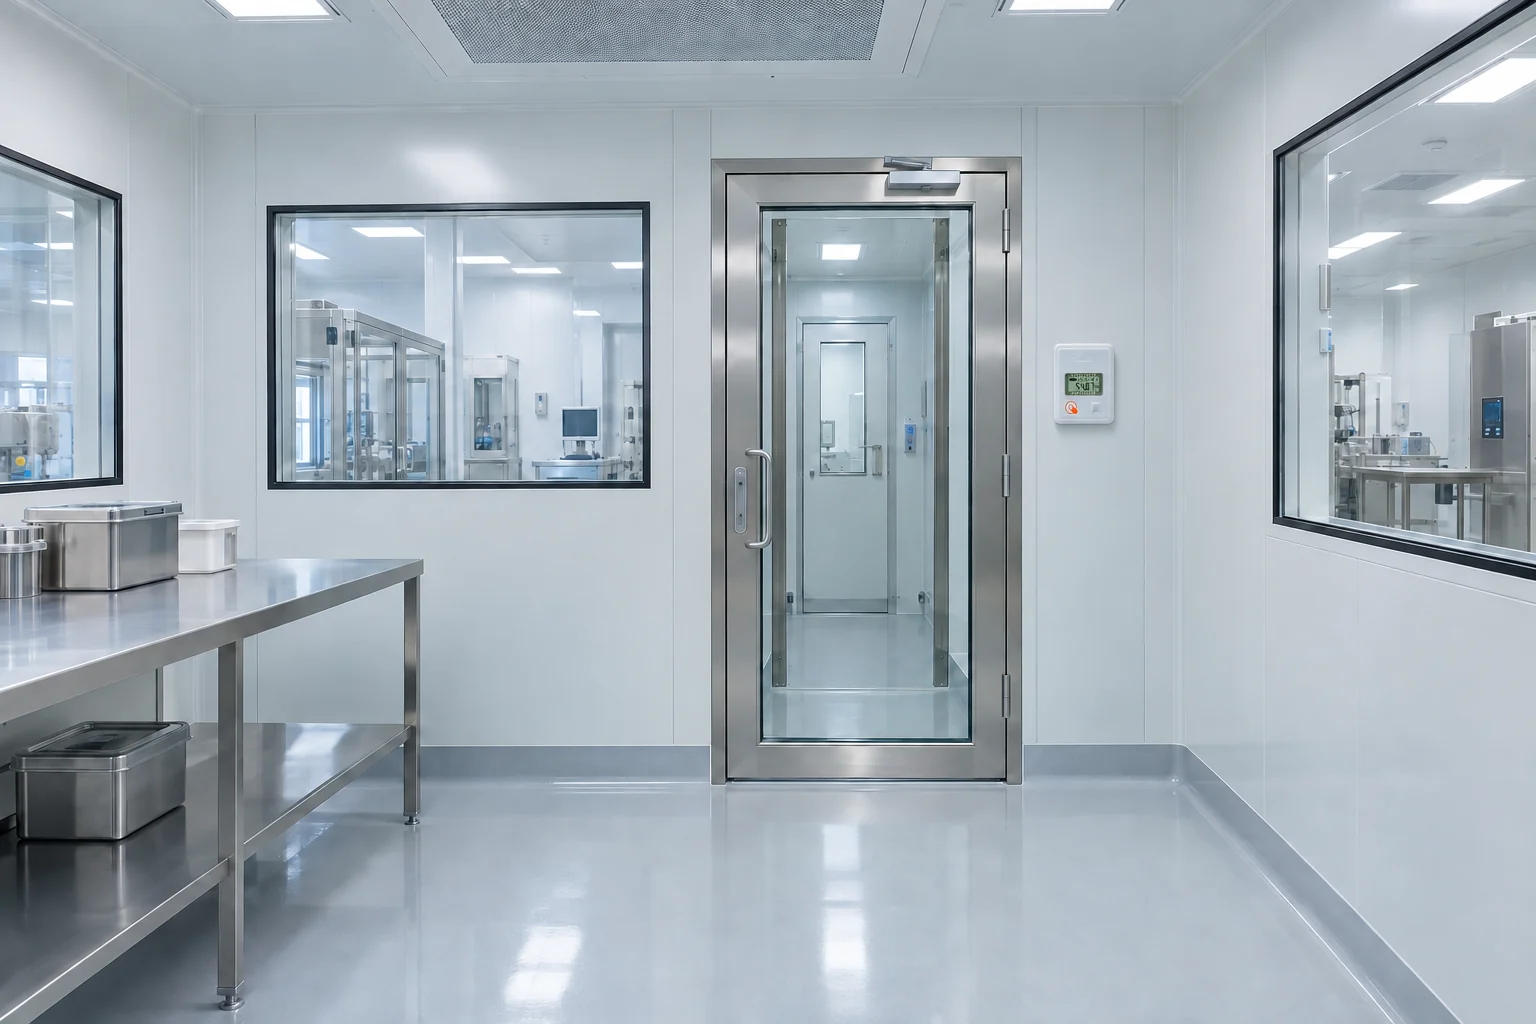
Why Cleanroom Monitoring Is Non-Negotiable
Cleanrooms are classified environments with strict controls over airborne particles, temperature, humidity, and air pressure. Even a brief deviation can affect product quality, testing integrity, or patient safety.
Without continuous monitoring, you risk:
- Batch failures caused by undetected temperature or humidity excursions
- Contamination events from pressure differential breakdowns
- Failed audits due to gaps in environmental data
- Product recalls triggered by out-of-spec manufacturing conditions
- Regulatory citations including FDA 483 observations and warning letters
The cost of a cleanroom excursion isn't just the product you lose—it's the investigation, the corrective action, the revalidation, and the reputational damage that follows. Monitoring prevents all of that by catching drift before it becomes a deviation.
What Does a Cleanroom Monitoring System Track?
Cleanrooms require multi-variable monitoring. Temperature and humidity are just the starting point. Depending on your classification and process, you may also need to track:
Temperature
Tight ranges are critical for pharmaceutical processes, semiconductor fabrication, and biological work
Relative Humidity
Affects product stability, static charge, and microbial growth potential
Differential Pressure
Ensures proper air cascade between classified and unclassified spaces
Particle Counts
Verifies that your room meets ISO 14644 classification standards
Airflow Velocity
Confirms HEPA and ULPA filtration systems are operating correctly
CO₂ and Gas Levels
Relevant for certain bioprocessing and cell culture applications
Qualified Controls builds systems that track every variable your process demands. All data flows into a single platform, so your quality team sees everything in one view.
How Our Monitoring Systems Work
We place calibrated sensors at critical points throughout your cleanroom—inside production areas, gowning rooms, airlocks, pass-throughs, and adjacent corridors. Each sensor reports readings at configurable intervals to our secure monitoring platform.
The platform continuously compares readings against your defined limits and sends alerts the moment a value moves out of range.
System features:
NIST-Traceable Sensors
Documented calibration histories and validated measurement accuracy
Continuous Data Logging
No gaps between readings with configurable logging intervals
Multi-Channel Alerts
Email, text, phone, and app notification for immediate response
Role-Based Access
Quality, operations, and maintenance teams see what they need
Automated Reporting
Daily reviews and audit preparation with formatted compliance reports
Tamper-Resistant Records
21 CFR Part 11 compliant audit trails and access controls
Data is stored securely in the cloud or on-premise, depending on your IT requirements. Every reading, alert, acknowledgment, and user action is logged with a permanent audit trail.
Meeting FDA, ISO, and GMP Requirements
Qualified Controls' monitoring systems are designed to satisfy the world's most stringent regulatory frameworks:
Pharmaceutical Manufacturing Control
Requires adequate controls over environmental conditions during pharmaceutical manufacturing
Electronic Records Integrity
Mandates electronic record integrity, audit trails, and access controls
Cleanroom Classification
Defines cleanroom classifications and monitoring protocols for airborne particles
Sterile Manufacturing
Sets stringent requirements for sterile manufacturing environments
Compounding Standards
Governs environmental monitoring for compounding pharmacies and hazardous drug handling
Medical Device Quality
Requires documented environmental controls for medical device manufacturing
When inspectors visit, they want to see continuous data, clear trend analysis, documented responses to excursions, and evidence that your monitoring system is validated and maintained. Qualified Controls makes that information accessible with a few clicks.
Cleanroom Classification Checker
Answer a few quick questions to get a personalized assessment of your cleanroom monitoring requirements and recommended ISO classification.
Pressure Differential Monitoring
Maintaining proper air cascade is one of the most critical aspects of cleanroom operation. Positive pressure keeps contaminants out. Negative pressure contains hazardous materials. Either way, the pressure relationship between rooms must be verified continuously.
Our pressure monitoring provides:
- Real-time differential pressure readings between adjacent spaces
- Alerts when pressure drops below or exceeds acceptable ranges
- Historical trending to identify HVAC performance degradation
- Visual dashboards that show pressure relationships across your facility map
Door openings, HVAC cycling, and filter loading all affect pressure. Our system catches these fluctuations in real time, giving your team the data to respond and the records to document compliance.
Alerts That Drive Action
An alert is only valuable if the right person sees it in time to respond. Our system delivers notifications through:
- Email alerts with full context—sensor name, location, reading, and threshold details
- SMS and phone call escalations for critical excursions
- Dashboard warnings for quality and operations personnel
- Escalation chains that bump unacknowledged alerts to supervisors
You define who gets alerted, under what conditions, and how quickly alerts escalate. Every alert, acknowledgment, and corrective action is recorded in the audit trail.
How Installation Works
We design each cleanroom monitoring system around your facility's layout, classification requirements, and operational workflow.
The process includes:
- Site assessment to identify monitoring points and sensor types
- System design with sensor placement maps and wiring plans
- Installation with minimal disruption to active operations
- Calibration and validation documentation
- Staff training on dashboards, alerts, and reporting
- Ongoing support including calibration scheduling and system updates
We work with your quality team and validation engineers to make sure the installation meets your qualification protocols, including IQ/OQ/PQ documentation where required.
Why Choose Qualified Controls?
Cleanroom monitoring is what we do. We understand the regulatory landscape, the engineering behind classified environments, and the urgency that comes with an out-of-spec reading. Our team builds systems that satisfy quality teams, pass audits, and keep your production on track.
You get:
- A system designed around your cleanroom classification and process needs
- Continuous multi-variable monitoring from a single platform
- Audit-ready records that align with FDA, ISO, and GMP requirements
- Responsive alerts that prevent excursions from becoming deviations
- A partner that understands regulated manufacturing
Technical Specifications
Covers all common pharmaceutical, biotech, and industrial monitoring scenarios
NIST-traceable calibration ensures regulatory compliance and data integrity
Every second to 5-minute increments, fully configurable per monitoring zone
Temperature, Humidity, Pressure, Particle Counts with extensible options
FDA 21 CFR Part 211/11, ISO 14644, EU GMP Annex 1, USP 797/800, ISO 13485
Compliant audit trails, access controls, and tamper-resistant logging
REM Platform Architecture
Cleanroom monitoring integrates into Qualified Controls' REM platform—connecting every classified space to a centralized compliance record that satisfies FDA, ISO, and GMP auditors with continuous data and validated documentation.
Industries We Serve
Qualified Controls has designed cleanroom monitoring systems for regulated facilities across these critical industries.
Pharmaceutical Manufacturing
GMP-compliant environmental monitoring for drug manufacturing facilities with FDA 21 CFR Part 211 alignment, Part 11 audit trails, and continuous multi-variable tracking.
Biotech & Cell Culture
Aseptic processing and cell culture environments monitored for temperature, humidity, pressure, and particle counts with validated documentation for regulatory submissions.
Medical Device Assembly
ISO 13485-aligned cleanroom monitoring for medical device manufacturing with continuous environmental data and validated quality records.
Semiconductor Fabrication
Precision environmental control monitoring for semiconductor fabs requiring tight temperature, humidity, and particle count specifications across classified production areas.
Compounding Pharmacies
USP 797 and 800 compliant monitoring for sterile and hazardous drug compounding with pressure differential tracking and automated compliance reporting.
Research & Aerospace
ISO-classified laboratory and aerospace cleanroom monitoring with multi-variable tracking, calibration management, and audit-ready documentation.
Learn More
Don't Let an Undetected Excursion Shut Down Your Production
Cleanroom conditions are too critical to leave to manual checks and spreadsheets. A monitoring system gives your team the visibility they need to maintain classification, protect product quality, and stay compliant every hour of every day.